 Share this page by mail
Gasketing - Anaerobic adhesives Bostik Born2Bond™
Final Advanced Materials offers a range of Bostik Born2Bond™ anaerobic adhesives, specially designed for Gasketing.
These single-component solutions are a cost-effective and efficient alternative to traditional pre-formed gaskets. They ensure total surface-to-surface contact for durable sealing that resists vibrations, extreme temperatures, and exposure to oils, solvents, and water. Flexible and robust, these adhesives are suitable for both installation and preventative maintenance.
Additionally, the Born2Bond™ GA-WL range is not classified as hazardous under the European CLP Regulation (1272/2008).
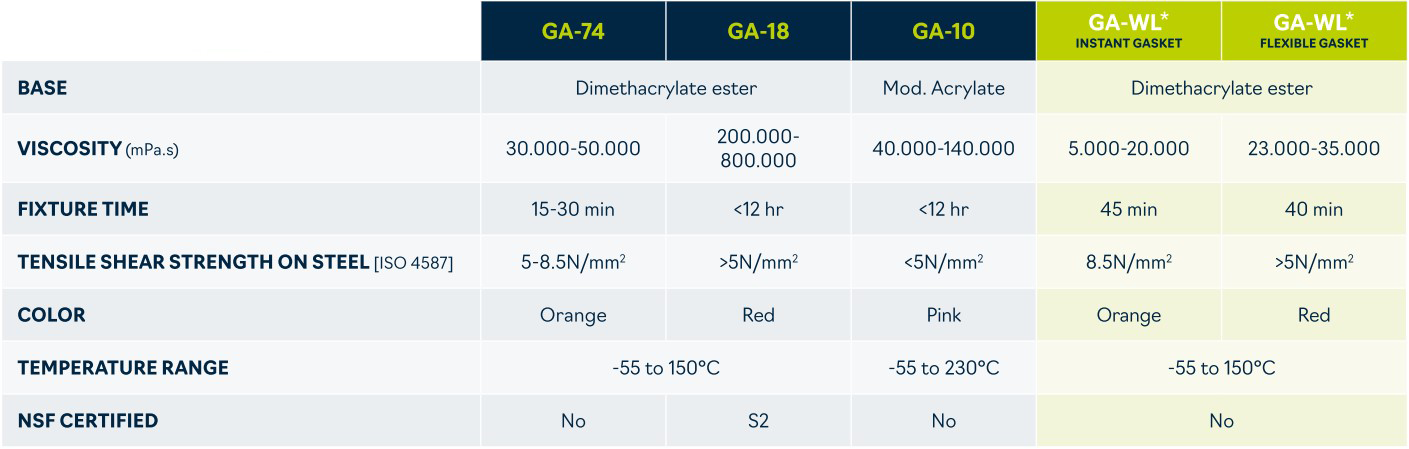
Details of our range GA-74, GA-18, GA-10, GA-WL instant gasket, GA-WL flexible gasket

Features of the gasketing adhesive:
- Outstanding fatigue strength
- Vibration resistant
- Corrosion prevention
- Prevents sagging and micro-movement
- Single component
- Variety of viscosities and strengths
- Instant and flexible seal options
- Suitable for active and passive metals
- Higher power transmission
The choice depends mainly on the temperature and the mechanical stresses. Final Advanced Materials' high-temperature epoxy resins are generally limited to between 150 and 350°C, with satisfactory mechanical resistance (typical sheer-stress 10–30 MPa) and a degree of elasticity. However, the ceramic cements produced by Final Advanced Materials can be used up to 2,200°C, depending on the grade (alumina, zirconia, silicate, silica). They have excellent temperature resistance, but remain fragile (brittle behaviour, no elasticity). In the case of assemblies subject to differential expansion or vibration, epoxy is by far the preferred solution, if permitted by the maximum temperature of the application. However, in the case of extreme environments (kiln, vacuum, reducing atmosphere) which exceed 350°C, ceramic cement must be chosen.
The ceramic cements distributed by Final Advanced Materials have maximum working temperatures ranging between 650°C and 2,200°C. For example, alumina-based formulations often reach 1,650–1,760°C in an oxidising atmosphere. However, silicate systems are limited to around 1,000–1,200°C. The real maximum working temperature depends greatly on the environment (air, vacuum, inert gas), the time of exposure to this temperature and the thermal cycle (gradient, thermal shock). Specifically: the metal-loaded ceramic adhesives produced by Final Advanced Materials resist only up to the maximum temperature of the filler (650°C, for example, in the case of aluminium powder).
Ceramic/metal assemblies require often very different coefficients of thermal expansion (CTE) to be controlled. Final Advanced Materials recommends alumina-, silica- or zirconia-based ceramic cements for temperatures >350°C, which can bond to all types of ceramics and, generally, metals. For intermediate applications (≤350°C), an epoxy resin loaded with alumina powder enables thermal stresses to be absorbed and will be very compatible with different expansion coefficients. The thickness of the bond line must be between 100 and 300 µm to limit stress. Surface pre-treatment (sanding, degreasing, etc.) greatly improves adherence and is absolutely necessary if the CETs are very different.
The Cotronics adhesives distributed by Final Advanced Materials have variable cycles.
In the case of a cement, initial drying at ambient temperature takes between 2 to 24 h, depending on the viscosity and thickness. A thermal aftertreatment can be performed to allow them to attain their optimum properties after firing. Excessively rapid drying can lead to cracking or porosity in the cement.
Final Advanced Materials' epoxy adhesives which resist up to 260°C must be cured at ambient temperature. Epoxy adhesives which resist up to over 300°C require heat curing.