 Share this page by mail
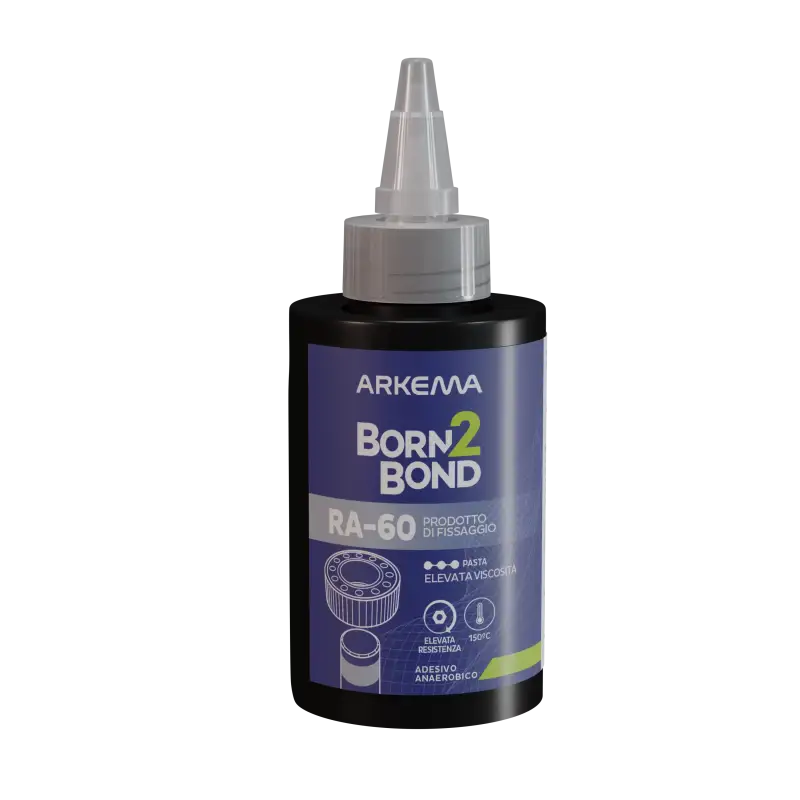
Retaining - Anaerobic adhesives Bostik Born2Bond™
Born2Bond™ Retaining anaerobic adhesives provide an effective, flexible, and sometimes complementary solution to mechanical fixing methods.
Designed to bond all types of cylindrical components, these single-component adhesives also seal metal joints, eliminating the risk of fretting corrosion. They ensure complete surface-to-surface contact, form a durable bond, and withstand vibrations, extreme temperatures, and chemical exposure.
The RA-WL product is not classified as hazardous under the CLP Regulation.
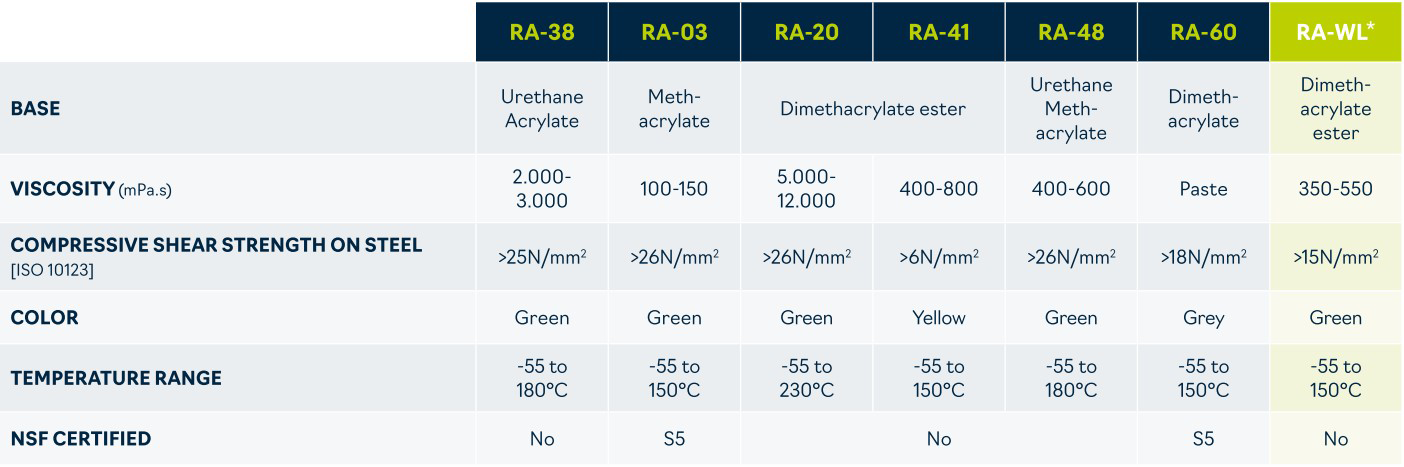
Details of the references RA-38, RA-03, RA-20, RA-41, RA-48, RA-60, RA-WL:
Retaining - Features:
- High power transmission
- Resistance to dynamic loads
- Vibration resistant
- Corrosion prevention
- Single component
- Variety of viscosities and strengths
- Suitable for active and passive metals

The choice depends mainly on the temperature and the mechanical stresses. Final Advanced Materials' high-temperature epoxy resins are generally limited to between 150 and 350°C, with satisfactory mechanical resistance (typical sheer-stress 10–30 MPa) and a degree of elasticity. However, the ceramic cements produced by Final Advanced Materials can be used up to 2,200°C, depending on the grade (alumina, zirconia, silicate, silica). They have excellent temperature resistance, but remain fragile (brittle behaviour, no elasticity). In the case of assemblies subject to differential expansion or vibration, epoxy is by far the preferred solution, if permitted by the maximum temperature of the application. However, in the case of extreme environments (kiln, vacuum, reducing atmosphere) which exceed 350°C, ceramic cement must be chosen.
The ceramic cements distributed by Final Advanced Materials have maximum working temperatures ranging between 650°C and 2,200°C. For example, alumina-based formulations often reach 1,650–1,760°C in an oxidising atmosphere. However, silicate systems are limited to around 1,000–1,200°C. The real maximum working temperature depends greatly on the environment (air, vacuum, inert gas), the time of exposure to this temperature and the thermal cycle (gradient, thermal shock). Specifically: the metal-loaded ceramic adhesives produced by Final Advanced Materials resist only up to the maximum temperature of the filler (650°C, for example, in the case of aluminium powder).
Ceramic/metal assemblies require often very different coefficients of thermal expansion (CTE) to be controlled. Final Advanced Materials recommends alumina-, silica- or zirconia-based ceramic cements for temperatures >350°C, which can bond to all types of ceramics and, generally, metals. For intermediate applications (≤350°C), an epoxy resin loaded with alumina powder enables thermal stresses to be absorbed and will be very compatible with different expansion coefficients. The thickness of the bond line must be between 100 and 300 µm to limit stress. Surface pre-treatment (sanding, degreasing, etc.) greatly improves adherence and is absolutely necessary if the CETs are very different.
The Cotronics adhesives distributed by Final Advanced Materials have variable cycles.
In the case of a cement, initial drying at ambient temperature takes between 2 to 24 h, depending on the viscosity and thickness. A thermal aftertreatment can be performed to allow them to attain their optimum properties after firing. Excessively rapid drying can lead to cracking or porosity in the cement.
Final Advanced Materials' epoxy adhesives which resist up to 260°C must be cured at ambient temperature. Epoxy adhesives which resist up to over 300°C require heat curing.